
Built to scale. Wired for innovation. Trusted to deliver.
Videomax’s manufacturing infrastructure is built to deliver both scale and quality. We operate two major production facilities in northern India, with a combined area of approximately 250,000 sq. ft.. Our newest facility, located in Greater Noida, Uttar Pradesh, spans multiple assembly lines and incorporates modern automation and process controls. This plant specialises in high-demand electronics such as LED televisions, power banks and audio systems, utilising state-of-the-art technology to achieve efficient, high-volume output. The factory is designed with flexibility in mind – quick changeover setups and modular lines allow us to adapt to different product types swiftly. Key production areas are maintained as clean-room environments, especially where sensitive electronic assembly is performed, ensuring minimal dust and contaminant exposure for better product reliability. Notably, both facilities are ISO 9001, 14001, 45001, 50001 & ISO/IEC 27001 Certified, reinforcing our adherence to quality management and environmental standards.


Cleanroom.
We operate an in-house Class 10,000 cleanroom (ISO-standard controlled environment) to ensure consistent quality and reliability. The controlled production zone includes a total of 2,000 ft² of regulated working space, with disciplined process control and inspection practices to maintain high manufacturing standards and quality.


Quality Control.
Our facilities boast 20+ NABL Certified advanced testing equipment supporting 40+ distinct tests conducted on-site. From Kashmir to Kanyakumari, our products are built to perform—because we test them like they’ll face the toughest real-world conditions. We use dust chambers, climate control chambers (temperature & humidity cycling), and salt-spray corrosion testing to validate durability across Indian and global climates. Vibration and drop tests simulate transport stress, while HiPot, leakage-current and insulation tests ensure electrical safety. Our anechoic testing fine-tunes audio output. Endurance rigs and thermal imaging verify reliability—so every unit ships robust, safe and consistent. Key testing and lab capabilities include:
 |  |  |
|---|---|---|
 |  |  |
 | 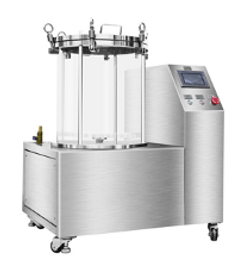 |
Our in-house testing laboratory is equipped with a comprehensive range of advanced instruments to validate product performance, safety, reliability and regulatory compliance across every stage of manufacturing.
Dimensional & Electrical Testing
Digital Micrometer, Digital Vernier Caliper, Digital Multimeter, LCR Meter, Digital MilliOhm Meter, Oscilloscope, Signal Generator, Variac (0–300V), Power Analyzer, Torque Meter & Weighing Machine.
Safety & Compliance Testing
Insulation Resistance Tester, Earth Continuity Tester, Leakage Current Tester, High Voltage (Hipot) Tester, High Voltage Tester, Surge Tester, Glow Wire Tester, Needle Flame Tester, Plug & Socket Tester & Burn-in Testing.
Environmental & Reliability Testing
Salt Spray Chamber, Dust Chamber, UV Aging Chamber, Temperature Controller, Heating Unit, Drop Tester, Drop Ball Impact Tester, Drip Test Setup, Vibration Test Machine, Connector Endurance Testing, Key Life Testing Machine & Corrosion Test.
Performance & Acoustic Testing
IR Thermometer, Thermal Imaging Camera, Air Flow Meter, Sound Level Meter, OmniMic Acoustic System, Anechoic Chamber, EMI/EMC Testing & Voltage Level Switching Jig.
Through these advanced testing facilities and a strong culture of quality, Videomax ensures that every product leaving our factories meets not only contractual specifications but also our own stringent engineering standards. Combined with skilled technicians, experienced engineers and internationally aligned quality systems, our infrastructure provides a reliable foundation for OEM,ODM & EMS manufacturing across consumer and commercial electronics.